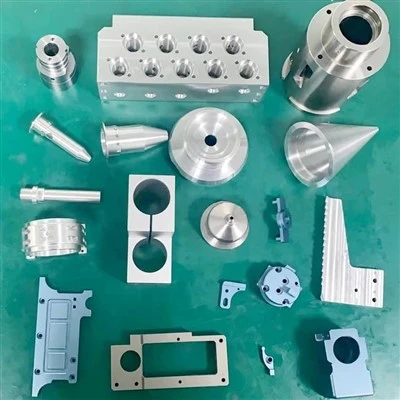
Precision-machined metal sleeves featuring tight-tolerance internal and/or internal-external concentric threads. Engineered for high-load mechanical interfaces, threaded insert reinforcement, and multi-axis alignment assemblies.
Core Capability: Concentricity TIR <= 0.005 mm; thread profile conformity per ISO/UN/ACME.
Production Scope: Made-to-print (OEM/ODM), prototype (FAI/PPAP) to volume scalable. Supplying tier-2/tier-3 industrial automation, fluid power, and EV sub-assemblies.
Technical Specifications
|
Parameter |
Standard / Range |
Test / Verification Method |
|
Material Grades |
316L / 303 / 17-4PH, 4140, 4140QT, Brass C36000, AL 6061-T6 |
Mill Test Certificate (EN 10204 3.1) |
|
Thread Standards |
Metric (ISO 6H/6g), UNC/UNF (Class 2A/2B, 3A/3B), NPT/BSPP on request |
Tri-roll thread comparator / Thread plug-ring gauges |
|
Outer Diameter (OD) |
DIA 4 mm - DIA 80 mm |
Micrometer / Air gauge |
|
Length Tolerance |
+-0.02 mm (Standard), +-0.005 mm (Precision ground) |
Height master / Optical comparator |
|
Concentricity (TIR) |
<= 0.008 mm (Standard), <= 0.005 mm (High-precision grade) |
CMM rotary axis / V-block indicator |
|
Surface Hardness |
HRC 28-32 (4140QT), HRC 38-43 (Nitrated / Induction hardened) |
Rockwell / Vickers hardness tester |
Key Features
Simultaneous ID/OD Turning: Single-setup multi-axis turning eliminates cumulative indexing error between external body and internal thread axis.
Thread Rolling vs. Single-Point: Rolled threads applied for dynamic fatigue resistance on structural alloy steels; single-point precision lathe boring applied for low-volume or abrasive stainless grades.
Anti-Galling Surface Finish: Controlled micro-finish (Ra <= 0.8 um) paired with optional dry lubricant (MoS2/WS2) or black oxide treatment to eliminate thread seizure in stainless-to-stainless mating.
Stress-Relieved Blanks: Thermal stress-relieving cycles applied post-rough turning on structural steels (> 4140) to prevent post-machining dimensional drift.
Typical Applications
Robotic Joint Housings: Preload spacer sleeves with concentric pilot diameters.
Hydraulic Manifold Blocks: High-pressure port adapter sleeves resisting cyclic pressure pulsation up to 350 bar.
EV Powertrain Gearboxes: Rotor shaft housing location sleeves subject to thermal expansion differential.
Customization Scope
Geometry: Flanged, stepped, slotted, oil-grooved (axial/spiral), or cross-drilled cross-holes.
Coatings: Passivation (ASTM A967 for 300 series), Zinc-Nickel (ASTM B841, 1000h+ red rust), Electroless Nickel (ENP, 10-25 um).
Identification: Laser-etched part number, heat lot code, or orientation index line.
Quality Control Protocol
First Article Inspection (FAI): AS9102 / PPAP Level 3 documentation package available upon request.
In-Process Control: Statistical Process Control (SPC) on critical OD/ID dimensions via automated air-gaging stations.
Final Audit: 100% Go/No-go thread gauging, optical surface defect inspection, AQL 1.0 sampling for dimensional CMM report.
Manufacturing & Facility Baseline
Equipment Line: 18 Citizen/Star Swiss-type CNC lathes (up to DIA 32 mm bar feed); 12 Miyano/Doosan 8-axis fixed-head turning centers (up to DIA 125 mm chucking); 3 Studer cylindrical grinders.
Quality Lab: Zeiss DuraMax CMM, Mitutoyo contour/surface roughness tester, optical thread profile projector.
QMS Compliance: ISO 9001:2015 certified floor with IATF 16949 process-compliant production controls (APQP, PPAP, FMEA, MSA, SPC implemented for automotive/EV lines); material traceability maintained from bar stock rack to final pallet.
Packaging & Logistics
Corrosion Protection: VCI (Volatile Corrosion Inhibitor) poly bag seal with desiccants for carbon/alloy steel parts; individual plastic matrix tray separation for precision-ground OD surfaces.
Lead Time:
• Prototype / FAI tooling: 12-18 business days.
• Volume production (5,000-50,000 pcs): 3-5 weeks rolling forecast / JIT release.
Shipping Terms: FOB / CIF / DDP (Air Express or Sea Freight palletized).
Quality Exception & Dispute Resolution
Non-Conforming Lot Protocol: 8D/CAR report issued within 48 hours of formal complaint.
Remediation: Immediate sorting/rework at destination or replacement air-shipped at manufacturer cost if root cause traces to machining drift.
Frequently Asked Questions
Request a Quote (RFQ)
Required RFQ Submission Checklist (< 24h technical feasibility & pricing turnaround):
CAD File: STEP / IGES format + 2D PDF with GD&T callouts for TIR and thread class.
Material Grade: Specific alloy or equivalent standard (e.g., AISI 4140, SUS 316L).
Volume Profile: Annual volume & release schedule (e.g., 10,000 pcs/year in 4 quarterly releases).
Compliance / Surface: Passivation, plating spec, PPAP Level 3 / AS9102 requirement.
Hot Tags: precision threaded sleeves, China precision threaded sleeves manufacturers, suppliers, factory